


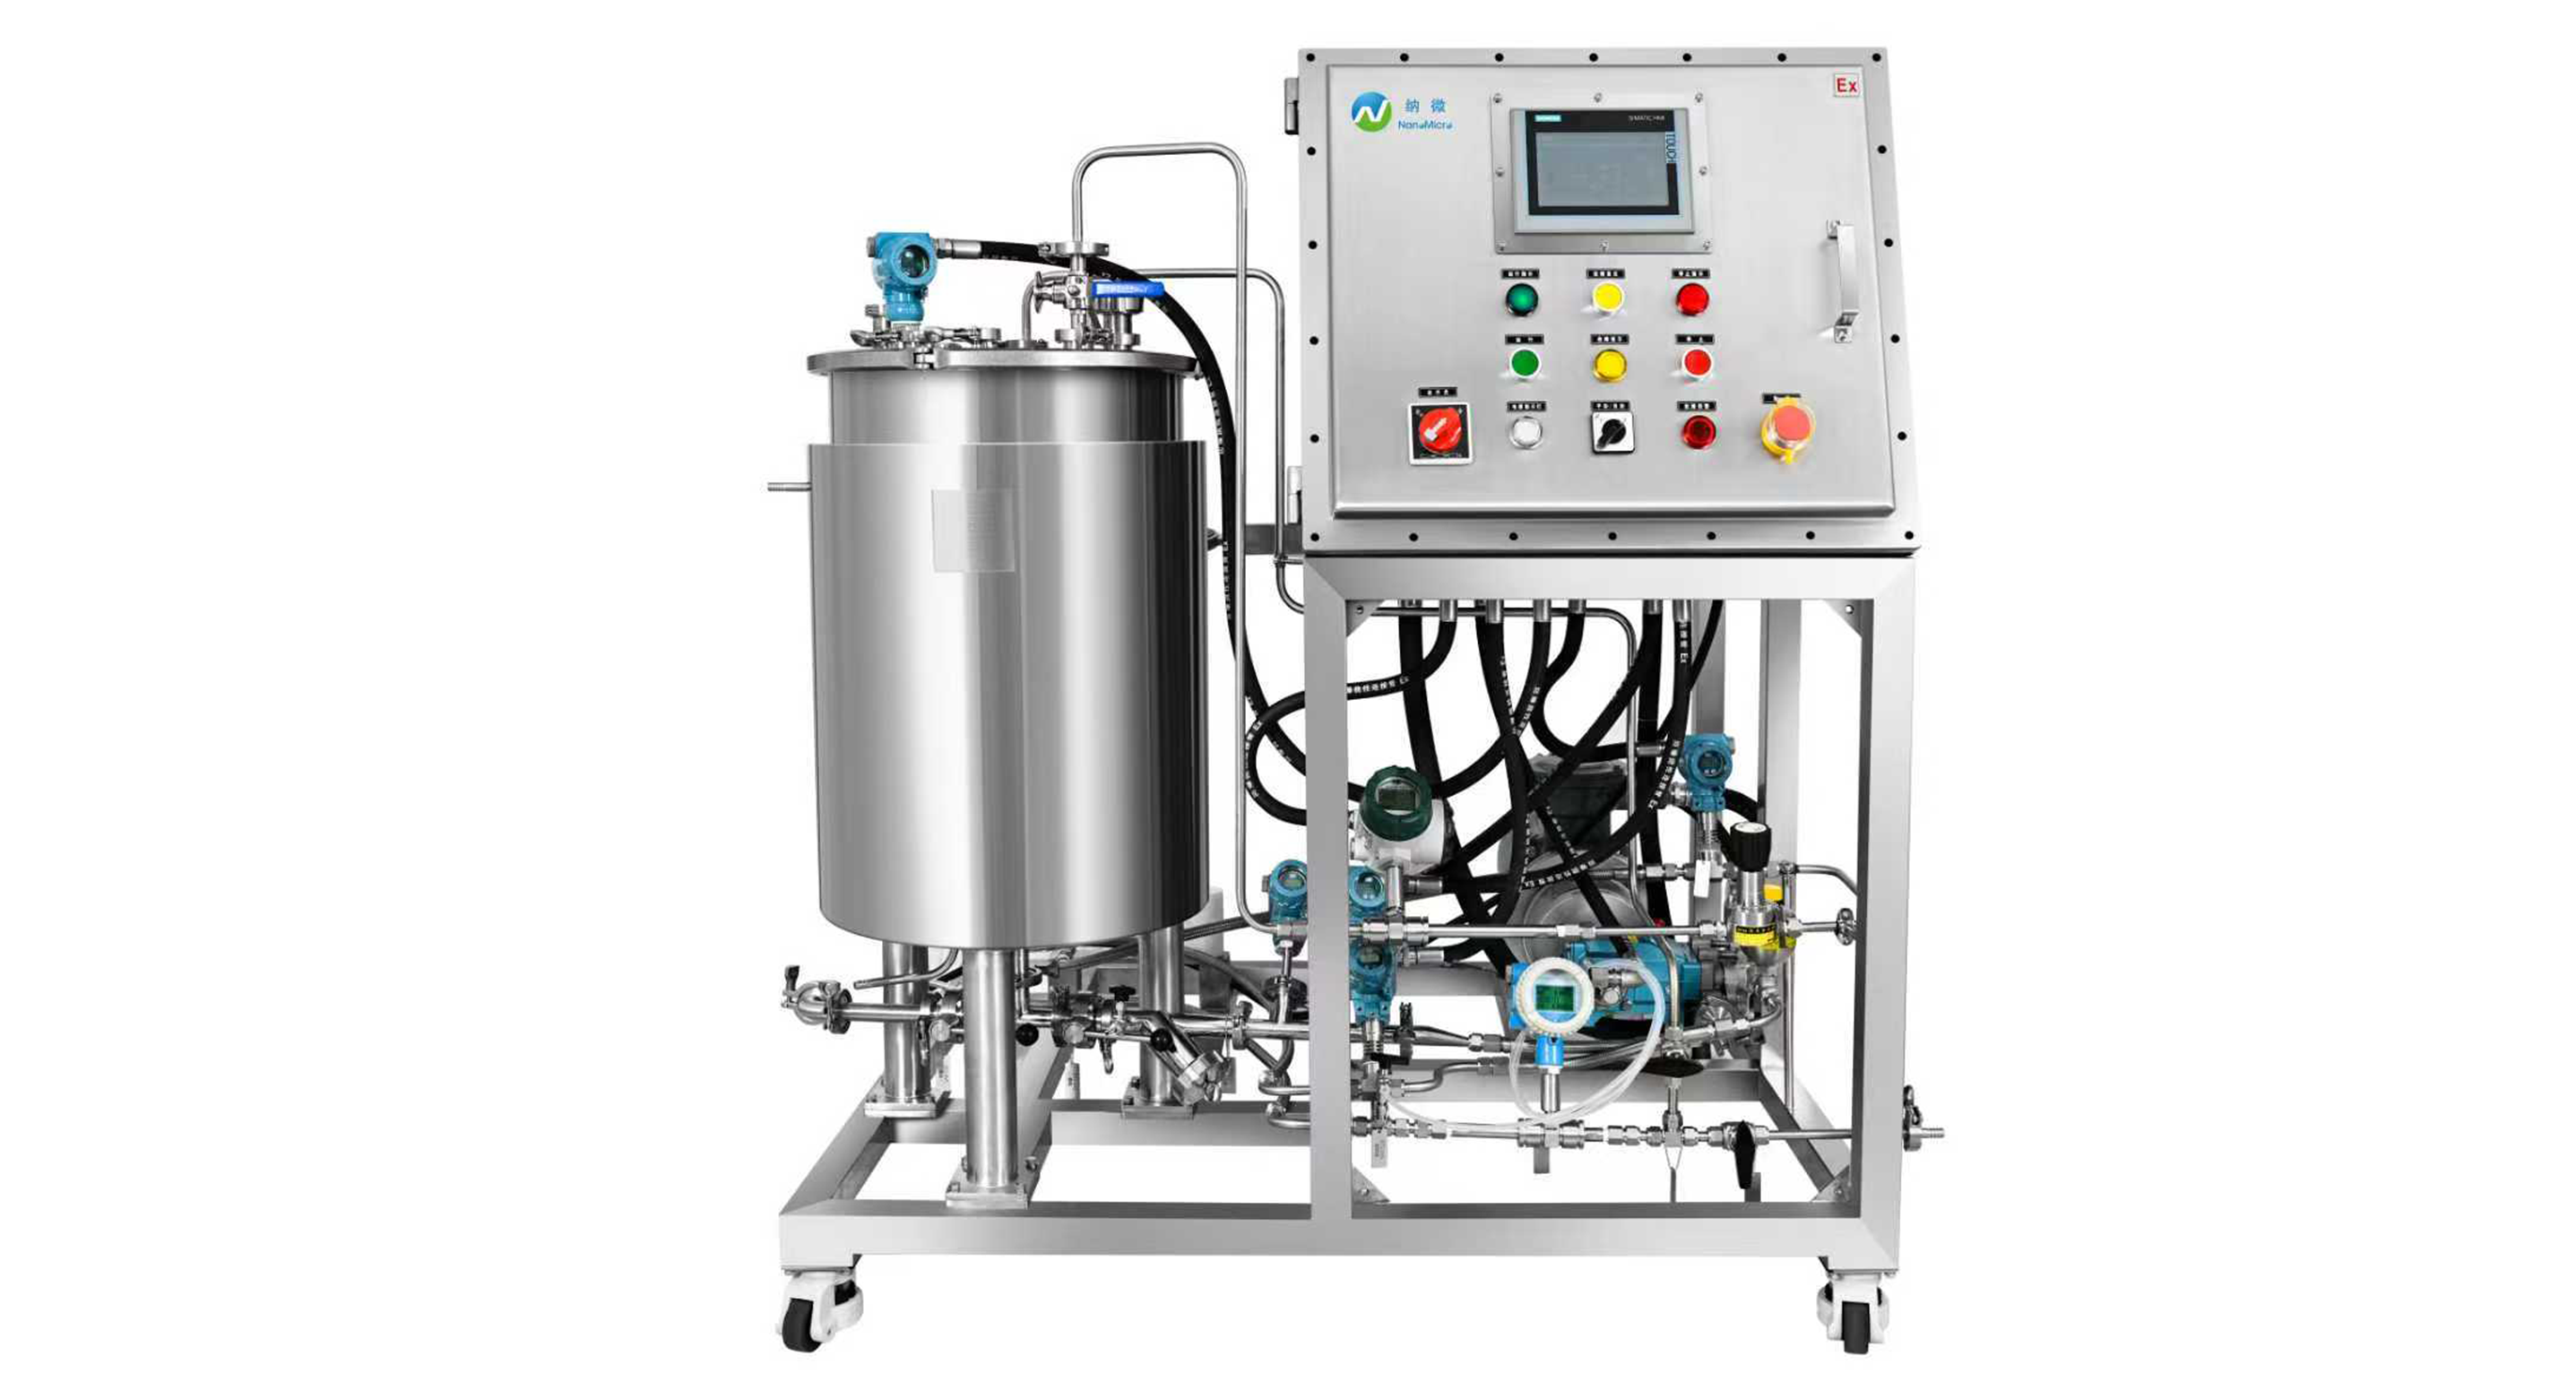
Material Concentration System
Our proprietary cross-linked polymer solvent-resistant membranes are designed for concentrating target product molecules in pharmaceutical manufacturing. They offer excellent fouling resistance and stable flux, with full-service support from process development to equipment delivery.
Product Description
Background:
The pharmaceutical industry consumes large volumes of organic solvents during reaction and purification processes. To address the dual challenges of environmental pressure and cost control, solvent recovery has become essential. Currently, pharmaceutical manufacturers primarily rely on distillation and rectification for solvent recovery, but these methods have significant limitations: high energy consumption, low efficiency, poor suitability for heat-sensitive materials, and safety risks associated with high-temperature operations. In contrast, membrane-based solvent recovery systems effectively overcome these limitations. These systems enable continuous solvent purification at low or ambient temperatures, support concentration of drug molecules in various solvent systems, and ensure compliance with relevant regulatory requirements.
Key Advantages:
Membrane-based solvent recovery systems not only enable continuous solvent purification at low or ambient temperatures but also support concentration of drug molecules in various solvent systems while ensuring regulatory compliance.
Compared to traditional thermal treatment, membrane technology offers the following advantages:
1. Reduced energy consumption: up to 80% energy savings compared to thermal methods;
2. Simplified process: 5-10x shorter processing time;
3.Solvent recovery: recovery rate exceeding 90%;
4.GMP-compliant design;
5. Highly automated, easy and safe operation.
Core Technology:
Nanotin leverages proprietary highly cross-linked polymer membrane materials, delivering exceptional chemical stability and high retention performance (molecular weight cut-off range of 120 - 700 Da). By precisely controlling membrane pore size at the molecular scale, our organic solvent-resistant membranes achieve efficient solute-solvent separation, enabling ultra-pure solvent recovery and concentration of target molecules in pharmaceutical applications. All wetted materials in the membrane system are carefully optimized to ensure optimal solvent stability. Additionally, the wide-channel design provides excellent fouling resistance, overcoming the challenge of rapid permeate flux decay commonly observed in traditional ultrafiltration membranes during concentration processes.
Methanol | Ethanol | Acetonitrile-Water | Hexane | Heptane | Ethyl Acetate | Xylene | Halogenated Alkanes | |
P Series | |
| | |||||
N Series |
|
|
|
|
|

Typical Solvent Resistance of Membranes
Our end-to-end solvent management platform integrates multiple unique advantages: broad pH compatibility, stable operation under demanding high-concentration solvent conditions, industry-leading solvent recovery efficiency, and full compliance with pharmaceutical GMP certification and fine chemical quality control requirements.

Solvent Recovery System
Product Overview:
P Series and N Series membranes are designed for polar and non-polar solvent systems, respectively. To ensure long-term, stable, and superior performance across different solvent systems, our membranes feature:
1. Excellent stability and low extractables in solvents
2. High solvent permeability
3. High retention of APIs
Typical Performance - Retention
API molecular weight,Da |

Note: Given the complexity of the solvent-solute-membrane ternary system interactions, we strongly recommend that users conduct performance validation with actual process feed streams.

Typical Applications of Membrane Technology in API Concentration and Organic Solvent Recovery
Application Example
Membrane concentration is the preferred technology for concentrating heat-sensitive pharmaceuticals. Given the stability of membrane products in organic solvents and molecular weight cut-off, selecting the right membrane can be challenging. Consider a cyclic peptide antifungal drug with a molecular weight of 1250. After purification, the solvent system is 35% acetonitrile-water with a concentration of approximately 5 g/L. Due to the insufficient solvent resistance of conventional filtration membranes, the feed must be significantly diluted before concentration. This additional dilution not only impacts process efficiency but also generates large volumes of waste liquid containing low concentrations of organic compounds, resulting in significant disposal costs.
Our P Series products can directly concentrate this drug in a 35% acetonitrile-water system, with a designed concentration factor of 10x. The membrane exhibits excellent retention performance, retaining nearly all of the material in the concentrate, with a retention rate of 99.8%. The membrane is fully compatible with this drug system, and no significant unknown impurities affecting drug purity were observed during the concentration process.

Ordering Information


